Risks unveiled:
Tackling the blindspot of
high-performance AM parts

Challenge
While tensile testing may be seen as the ‘gold standard’ for mechanical property insights, it has notable limitations when it comes to testing on complex geometries, as commonly seen in additive manufacturing (AM).
As part of the optimisation process, these geometries often undergo topological optimisation using extensive finite element modelling. A key input of this modelling process is the mechanical property data of the material making up the part. Typically, this data is obtained by performing uniaxial tensile testing on separately printed witness coupons, which are assumed to represent the entire component’s properties. However, this assumption overlooks a critical factor: the thermal history of a part depends on its geometry.
Consider a thin section of a part. Because it cools faster than thicker sections, its thermal history differs, leading to potentially significant variations in microstructure and mechanical properties across the part. This effect is particularly pronounced in the complex geometries common in additive manufacturing.
While data from witness coupons may suggest uniform mechanical properties, the actual part may have undetected variations, potentially increasing the risk of failure.
Objective
The aim of this case study, conducted in conjunction with Alloyed, was to use Profilometry-based Indentation Plastometry (PIP testing) to compare the mechanical properties of a metal 3D-printed part to those of a witness coupon.
Witness coupons present challenges. While they provide a window of mechanical performance, the information obtained through witness coupons is only related to the gauge section of the coupon and its specific location within the AM build. As a result, they may not accurately represent mechanical performance over the entire length of the coupon or the geometry it is intended to represent.
It is also worth noting that coupons are often produced and tested to determine the expected performance capabilities of specific material and process combinations. This means that the test results aren’t always reliable as the geometric factors, print orientation and thickness of the coupon might not be representative of the final, produced part. This lack of correlation provides inconsistencies in the mechanical performance of a part versus expectation.
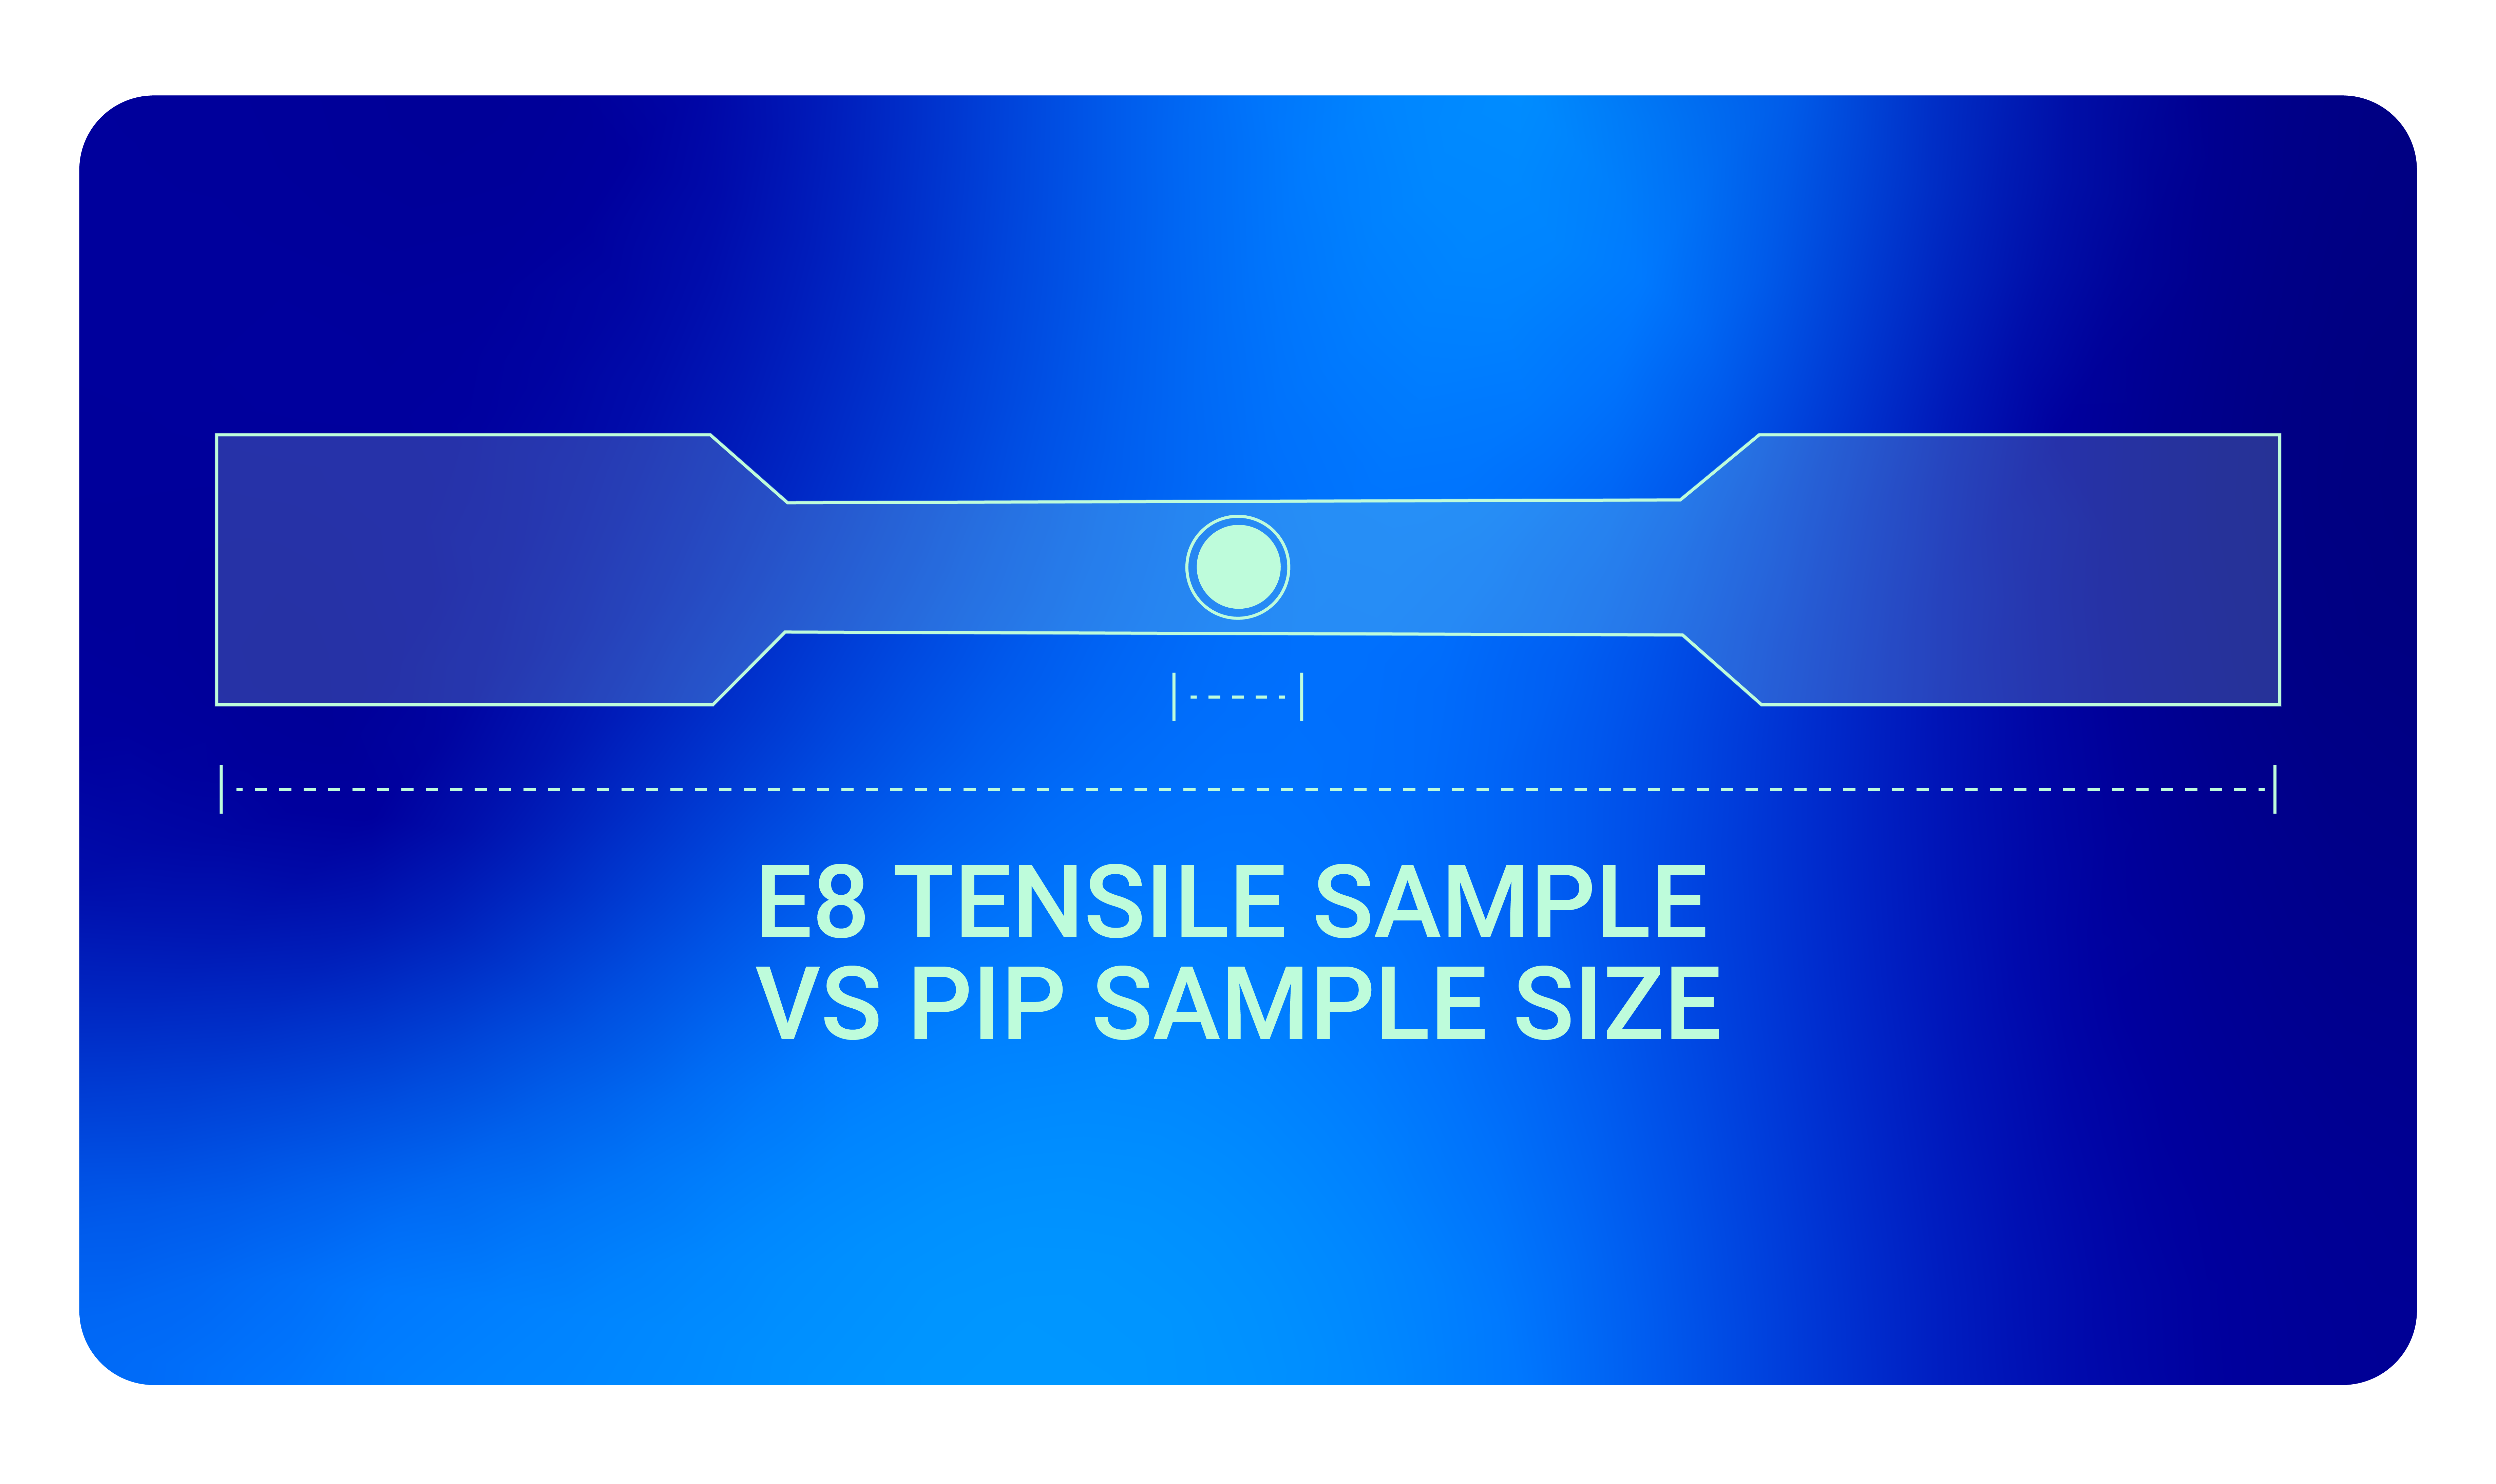
This study explores the possibility and importance of analysing materials in their true form to gain a deep understanding of the relationship between process, geometry, and materials. Unlike tensile testing, PIP can test small, un-machined samples from the final part, eliminating the uncertainties associated with witness coupons. By providing the ability to characterise property changes in complex geometries, PIP allows designers and engineers to optimise performance and increase confidence in part reliability.
Materials
The automotive bracket and associated vertical tensile coupons used in this case study were printed in AlSi10Mg . The sample was provided by Alloyed, designed by Gestamp, and manufactured using laser powder bed fusion.
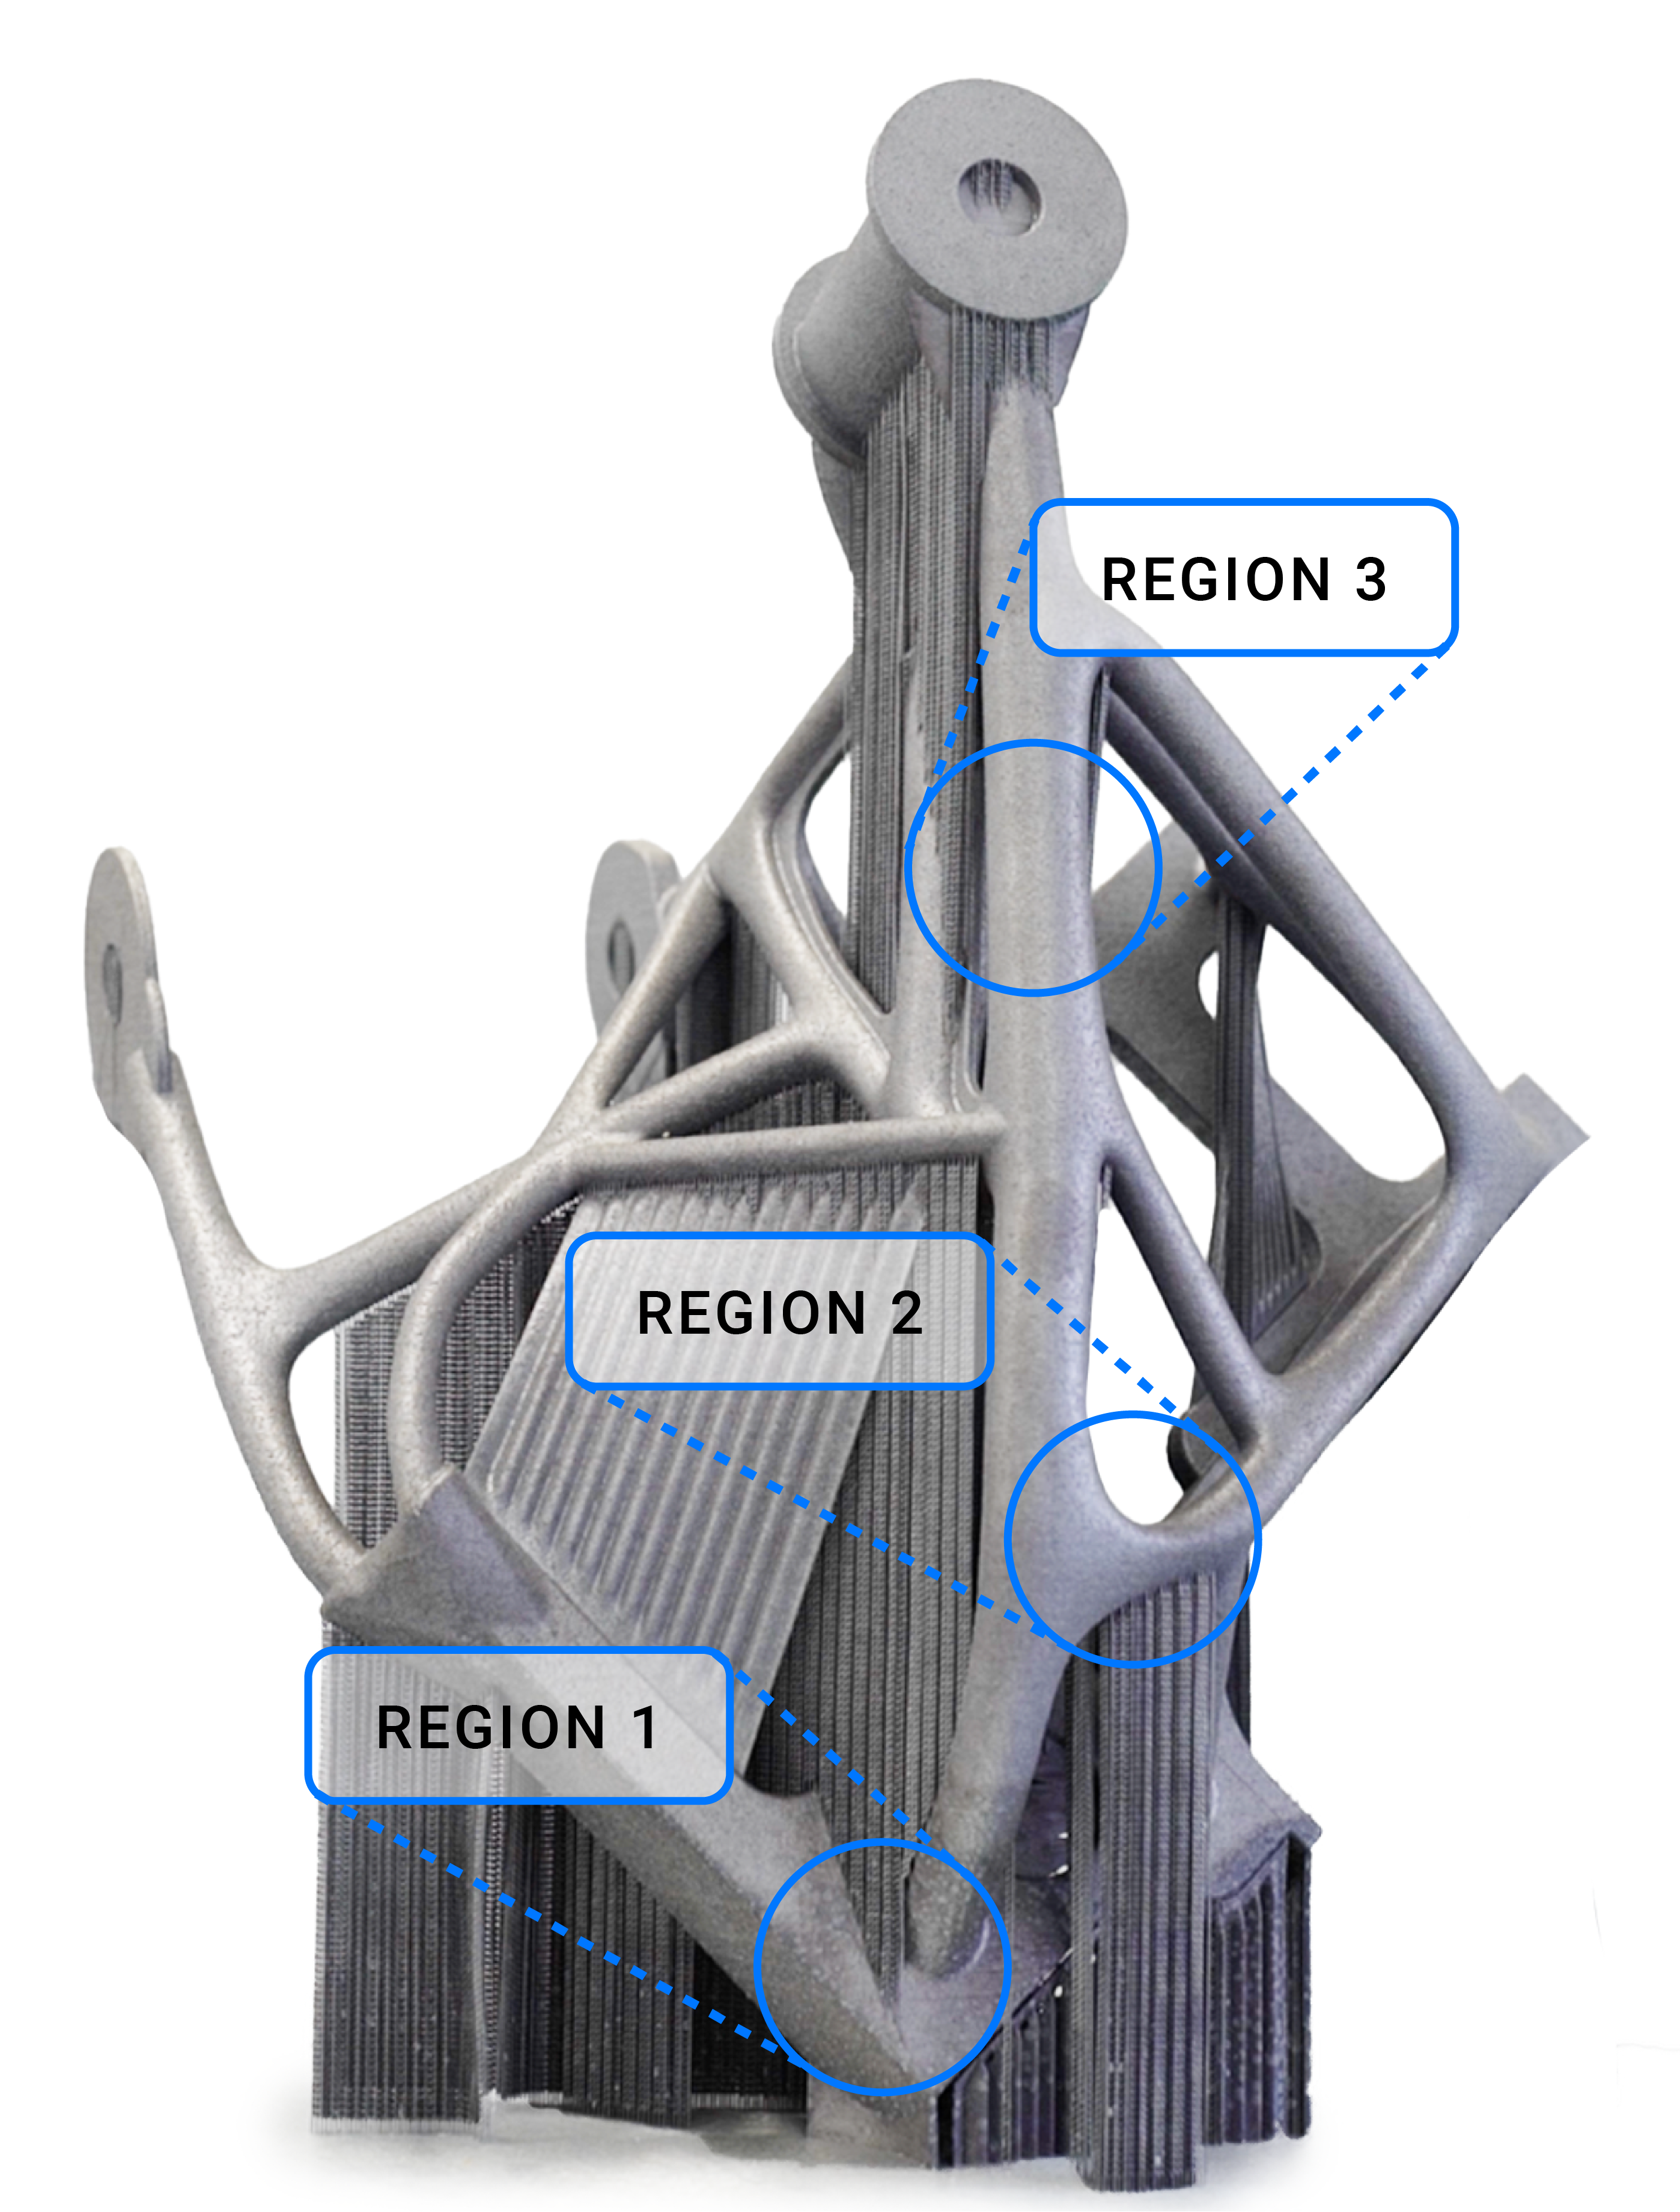
The automotive bracket was investigated in three different regions (Figure 1) undergoing typical LPBF environmental circumstances that could affect the local mechanical performance:
1. Close to the build plate, which could see the highest magnitude of annealing in a longer build.
2. Aggressive downskinning, in which parameters are often adapted and defects, high residual stresses and distortions are more common.
3. Vertical section further fromthe build plate, which could represent the bulk and therefore the expected baseline which would be investigated by extracting a coupon.
Measurements
The mechanical properties (stress-strain relationships) of both the witness coupon and AM part were measured using a PLX-Benchtop, a compact system that delivers mechanical testing data from an automated indentation test. The technology uses the novel PIP method, developed by former University of Cambridge materials scientists at Plastometrex. PIP uses an accelerated inverse finite element method to infer accurate stress-strain curves from indentation test data.
The PLX-Benchtop comes with three indenter tip sizes, allowing stress-strain measurements to be taken as close as 5 mm, 2.5 mm, and 1.5 mm apart. The test itself is fully automated and takes less than 5 minutes without the need for separate coupons or extensive sample preparation.
In this study, the larger diameter indenter (1000 µm) was used to test the as-built sample. Indentation was performed parallel to the build direction to produce radially symmetric indents for the inference of stress-strain curves . The part was sectioned and prepared to a 1 μm diamond finish prior to indentation in the different regions.
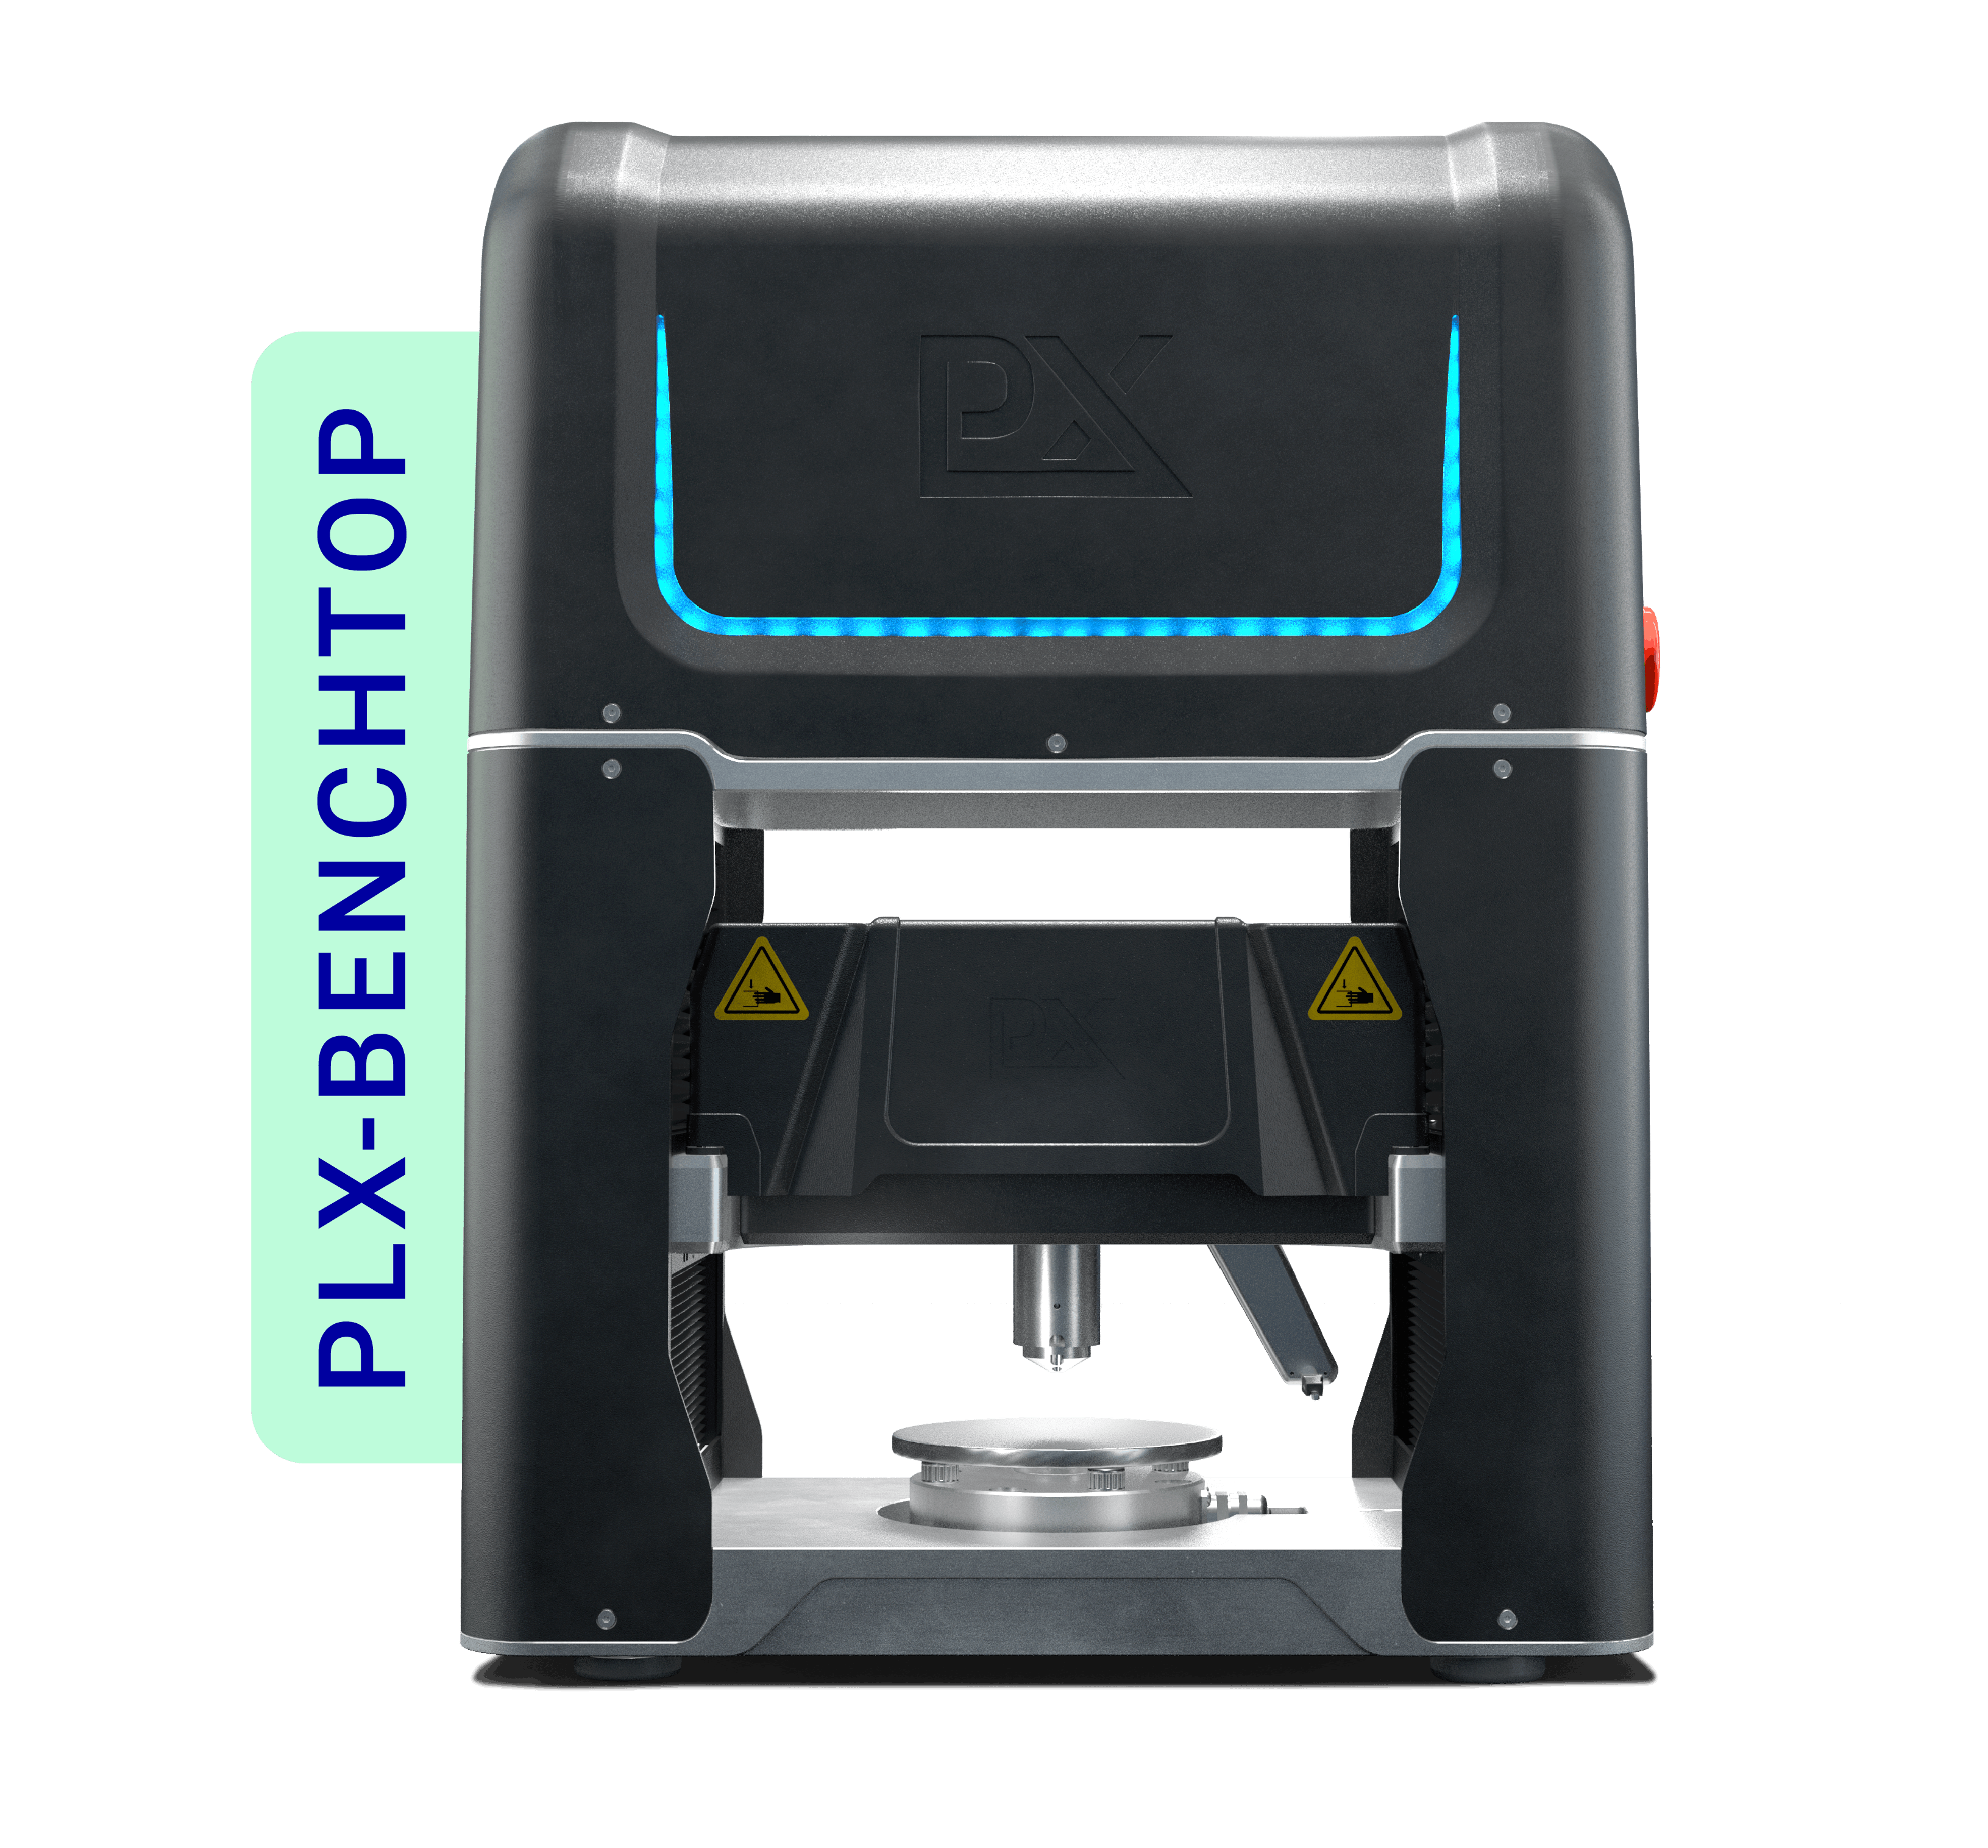
Figure 2: The witness tensile coupon was tested using uniaxial testing and PIP testing, minor differences between these results are attributed to the anisotropy confirmed to be present in the sample. PIP testing was used on different regions of the printed part.
Results
In this case study, we compared results from uniaxial tensile testing with those obtained from PIP tests (Figure 2) to determine whether testing on a witness coupon provides representative data of an additively manufactured part.
So, did the results from testing done on the coupon tell the same story as those done directly on the part itself? With a variation in mechanical properties of almost 20% in different locations, certainly not.
The PIP testing performed on the additively manufactured automotive bracket across the specified regions yielded some interesting results. The curve from Region 2, characterised by aggressive downskinning, shows a significant (>10%) reduction in UTS as compared with Regions 1 and 2.
Figure 3: PIP testing shows that different regions of the part show different mechanical behaviour.
Figure 4: PIP testing on the witness coupon shows differences in behaviour between the witness coupon and the part itself.
Previous work by Plastometrex has indicated that distance from the build plate can influence mechanical properties, however the similarity in results between Regions 1 and 2 suggests minimal inhomogeneity along the build direction. This was confirmed by testing at different build heights from the witness coupon. The reduced performance of Region 2 could stem from microstructural changes within the build. Additionally, the increase in effective annealing heat treatment time could provide an explanation for the lower yield of Region 1 as compared to Region 3.
It is important to note that the stress-strain curves inferred from these regions (Figure 3) will be influencedby the properties in the transverse directions as well as the build direction. These multi-directional inputs can only be obtained using a PIP test, whereas a single uni-directional tensile test would yield less comprehensive results.
Plotting the results from the testing of the part alongside the testing of the witness coupon (Figure 4) shows that the mechanical behaviour in different regions of the part can differ significantly from that of the witness coupon. Notably, the witness coupon aligns closely with the results from Region 3, attributed to its similar printing conditions. The discrepancies in other regions highlight the need for testing directly on printed parts for full confidence in their mechanical properties.
Conclusion
This study highlights the limitations of relying solely on witness coupons to assess the mechanical properties of 3D-printed parts. Current reliance on mechanical property data from witness coupons may not accurately represent the whole component. This is because the mechanical behaviour across regions can vary significantly. Consequently, reliance on data obtained from witness coupons can result in AM parts literally “cracking under pressure” in industries such as automotive, defence, and aerospace, where failure can be nothing short of catastrophic.
PIP testing offers a crucial advantage by enabling direct characterisation of additively manufactured parts across multiple locations.
This capability allows for more informed component modelling and ensures confidence in a part’s mechanical strengths across different regions.
While PIP testing is both faster and cheaper than traditional AM mechanical testing methods, it’s true value lies in the insights it provides. With the ability to extract accurate mechanical data from parts and samples, untestable with tensile, R&D teams can adopt more informed design strategies that optimise properties in specific regions. This leads to increased efficiency and cost savings in the additive manufacturing process while also resulting in reliable parts that meet stringent performance requirements.